 Skip to content
Manufacturing Network for Custom Tire Cover Programs
Szoneier routes each program through the manufacturing functions best suited to its product, material, artwork, volume and risk profile.
- 500-piece graphic programs can separate printing from bulk cut-and-sew
- 5,000-piece 600D programs use planned material, printing, assembly and QC stages
- 10,000-piece RV programs require bulk routing and staged controls
- Core materials are normally supported by at least 2 approved suppliers
One Network, Not One Universal Production Line
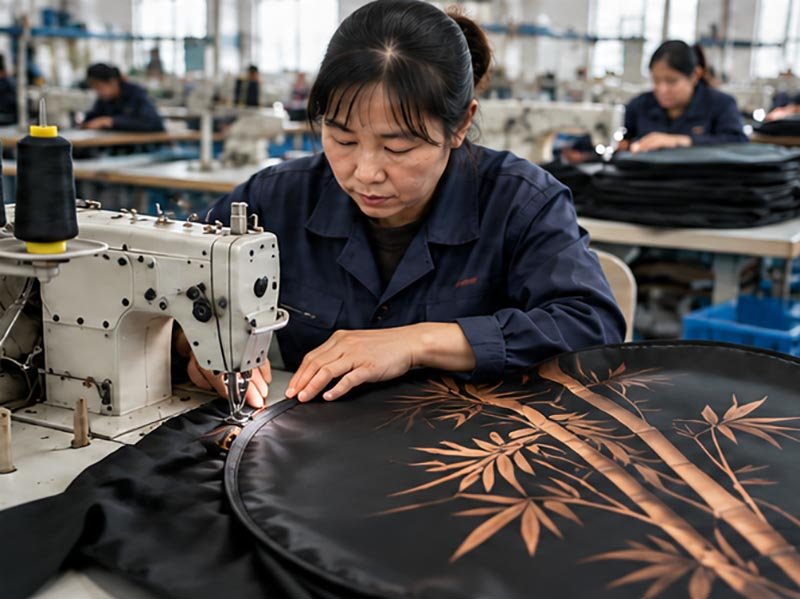
A custom tire cover can look simple from the outside, yet the manufacturing route changes considerably when the project moves from a standard printed cover to a new vehicle application, a backup-camera structure, a 600D RV program or a multi-SKU private-label collection. Szoneier manages these differences through an integrated manufacturing network rather than forcing every order through one identical production sequence.
Specialized Work Is Routed to Specialized Functions
Routing Starts With the Product Definition
One Customer Window Controls the Program
For the customer, the network is managed as one Szoneier program. Project management connects quotation assumptions, material approval, artwork revisions, pattern data, samples, QC requirements, packaging and shipping instructions. Internal routing can change as a project develops, but the approved customer requirement remains the controlling reference. This matters when a project contains multiple SKUs or when one process has a different production lead time from another. A network only creates value when the customer does not have to manage the handoffs personally.
Different Programs Take Different Production Routes
Szoneier does not assign every custom tire cover to the same route. The examples below show how product risk, quantity, artwork, material and vehicle requirements change the sequence. Final routing is confirmed only after the actual program inputs are reviewed.
| Program Example | Typical Routing Logic | Main Control Point | Why the Route Changes |
|---|---|---|---|
| New camera-compatible vehicle cover | Requirement review → fitment → pattern → prototype → camera verification → Golden Sample → bulk replication | Approved fitment and Golden Sample | Vehicle, tire, carrier and camera geometry must be proven before volume |
| 500 pcs full-color spare tire covers | Artwork/prepress → material/print → cut/sew/assemble → final QC → packing | Print registration and finished appearance | Full-color graphics require controlled print-to-pattern alignment before assembly |
| 5,000 pcs 600D printed covers | Material planning → print → bulk cutting → sewing/assembly → inline QC → final QC → packing | Material lot, first piece and process stability | Repeated output magnifies small cutting, sewing or print errors |
| 10,000 pcs RV 4-pack program | Material reservation → logo/print as required → efficient bulk cut/sew → multi-size QC → set packing | Size/SKU control and packaging accuracy | Large multi-pack orders depend on repeatable sizing and correct set configuration |
| Multi-SKU private-label collection | Project/SKU setup → material/artwork approvals → routed production → QC → branded packaging → shipment | Version control across SKUs | The commercial risk is mixing correct components into the wrong SKU or pack |
New Products Are Proven Before They Are Scaled
Requirement Definition Comes First
Development begins by separating confirmed information from assumptions. Depending on the product, Szoneier may review the tire sidewall, actual tire diameter, tire width, vehicle year, spare carrier, backup camera, artwork, target material, closure structure, packaging and expected order size. A new vehicle request described only as “fits Bronco” is not complete enough for engineering. Tire size and camera/carrier information may change the physical pattern. A photo, tire sidewall and rear-spare image can therefore be more valuable than a generic model name.
Pattern and Fitment Convert Data Into Geometry
Sampling Is a Risk-Reduction Stage
A standard OEM or printed sample can typically be planned at about 3-5 working days after requirements, material and artwork are confirmed. Camera-compatible samples are commonly about 5-7 working days. A new construction involving a new pattern, new material behavior or multiple revisions can require about 7-12 working days. These are planning references, not unconditional promises. The important output is the approved construction and Golden Sample that production can repeat.
Bulk Starts From the Approved Result
Material and Printing Are Routed as One Decision

The Substrate Changes the Production Route

Artwork Complexity Changes the Process

Approval Comes Before Repetition
New material/print combinations can require adhesion, scratch, fold, flex, color or other relevant checks before the route is approved. The goal is not to prove that a printer can place ink on the surface; it is to confirm that the finished graphic remains appropriate for the product’s material and handling. Once approved, material identity and artwork version become part of the controlled project record so the same route can be repeated on later purchase orders.
Bulk Cut and Sew Begins With an Approved First Piece
Material Release Before Cutting
Cutting Protects Fit and Graphic Position
Sewing Turns Geometry Into Repeatable Shape
Sewing controls seam width, stitch length, panel alignment, binding, elastic, reinforcement and final shape. A common main-seam stitch range can be around 3-4 mm, adjusted when heavy materials or special structures require another setting. Coated materials also need attention to needle density because excessive perforation can weaken the substrate.
First Piece Before Full Output
The first production piece provides a physical comparison against the Golden Sample and current specification. If material, pattern, printing setup, camera jig or construction changed, the first piece becomes an additional release gate before the line accelerates.

One Project Record Follows the Work
An integrated manufacturing network only works when every function is acting on the same approved information. Szoneier uses project-level records to connect commercial requirements with the material, artwork, pattern, QC and packaging references used in production.
Project ID Is the Main Link
A formal program can connect:
- Customer ID
- Project ID
- SKU
- Tire size and vehicle data
- Material ID and material lot
- Artwork version
- Printing process
- Pattern revision
- Camera version where applicable
- Golden Sample
- QC standard
- Packaging specification
- Shipping instruction
The value is practical. If artwork changes after the first sample, the new file must be visible to printing and QC. If a tire size changes, the pattern and sample may need review. If packaging changes, the product can remain technically correct while the final shipment becomes commercially wrong unless the packaging version is also controlled.
A Network Should Not Depend on Memory
Long-serving employees bring valuable experience, but a brand program should not depend on one person’s memory of what happened six months ago. Project records allow teams to reopen the approved product when a repeat order returns or when a quality issue needs investigation.
This becomes especially important for multi-SKU programs. Two covers can share the same material and look almost identical while using different artwork, tire size or packaging. The project record helps keep those differences explicit.
Customer Approval Remains the Controlling Reference
Internal production convenience does not override what the customer approved. If the material, pattern, print route, camera structure or packaging changes materially, the change can trigger additional review, first-piece verification or customer approval depending on risk.
Semi-Finished Transfers Stay Identified and Traceable
What Can Move Between Functions
Required Transfer Information
- Project ID
- Customer
- SKU
- Material lot
- Artwork version where relevant
- Quantity
- QC status
- Next process
QC Status Travels With the Product
The next process should know whether the previous process released the work. A printing defect should not be hidden by sewing; an unapproved cut panel should not become a finished product simply because assembly capacity is available. This creates a simple but important rule: movement does not equal acceptance. Each stage receives identified work and owns the checks required before adding more value.
Process Quality Has Clear Ownership
Material and Print Quality
Cutting, Sewing and Assembly Quality
Development Quality
Customer Specification Control
Szoneier project management keeps the overall customer requirement aligned across the network. The responsibility is broader than checking one process. It ensures the final manufactured product is the product the customer actually approved: correct material, correct fit, correct artwork, correct construction, correct quality standard and correct packaging. For bulk programs, final acceptance can follow the customer’s inspection plan or AQL requirements. Szoneier’s internal default framework can use General Inspection Level II with Critical 0, Major 1.5 and Minor 2.5 when another plan has not been agreed, while customer standards take priority.
The Approved Specification Overrides Local Convenience
Material Changes Are Reviewed
Artwork and Pattern Versions Stay Linked
Packaging Is Part of the Product Definition
Convenience Never Replaces Approval
Internal routing can change to protect schedule or capacity, but the route must still reproduce the approved product. The manufacturing network exists to create options without weakening control.
Primary and Backup Capability Reduce Supply Risk
Backup Is Not Random Re-Routing
Critical Functions Need More Than One Option
When Backup Routes Can Be Used
- Equipment breakdown
- Capacity overload
- Urgent delivery requirement
- Material delay
- Staffing constraint
- Packaging bottleneck
Risk Control Is a Procurement Value
Large brands rarely judge a manufacturer only by normal-day performance. They also want to know what happens when a machine fails, a supplier delays material or a best-selling SKU needs an urgent replenishment. A managed backup route gives the project team options before the issue becomes a missed shipment.
Capacity Is Routed by Bottleneck, Not Averaged
Szoneier uses a modular production-planning approach rather than dividing every order evenly across the manufacturing network. Development, printing, cutting, sewing, QC and packaging have different bottlenecks, so capacity planning starts by identifying the process that controls the schedule for the actual program.
High Volume Changes the Planning Logic
A 500-piece printed program can often be managed as one clear batch. At 5,000 or 10,000 pieces, material reservation, print throughput, cutting efficiency, sewing-cell balance, QC frequency, packaging supply and shipment staging become more important. Large orders therefore receive a production route rather than a simple “pieces per day” assumption.

Planning References by Order Scale
| Order Scale | Typical Planning Reference | Main Network Consideration |
|---|---|---|
| 100 pcs | About 7-10 working days | Approved sample, material and packaging readiness |
| 500 pcs | About 10-15 working days | Print/cut/sew balance and SKU complexity |
| 1,000 pcs | About 12-18 working days | Stable material, first-piece release and inline QC |
| 5,000 pcs | About 20-30 days | Material booking, production cells, packaging and staged QC |
| 10,000 pcs | About 30-40 days | Capacity allocation, bottleneck planning and shipment strategy |
| 50,000+ pcs | Rolling production + partial shipment | Material reservation, phased capacity and planned partial releases |

Peak Demand Uses Controlled Expansion
When demand rises, Szoneier can add sewing cells or shifts, move eligible work to approved backup capacity, protect development resources for urgent/high-value programs and adjust production sequencing. The objective is to increase usable capacity without mixing technically incompatible products into the same route.
Multi-SKU Brand Programs Need Network-Level Control
SKU Planning Before Production
Private Label Extends Beyond the Cover
Packaging Must Follow the Same Version Discipline
Forecasts Improve Routing
A brand that shares annual or seasonal forecasts gives Szoneier more opportunity to reserve material, plan repeatable SKU routes and separate development work from replenishment work. Forecasts do not remove the need for purchase-order confirmation, but they improve network planning around likely demand.

Repeat Orders Reopen the Approved Manufacturing Route
The manufacturing network is most valuable when it can reproduce an approved SKU months after the first launch. Szoneier treats repeat production as a controlled restart of the approved product rather than permission to make something generally similar to the previous order.
Reopen the Approved References
A repeat order can retrieve:
- Approved material and material specification
- Pattern revision
- Artwork version
- Color reference
- Camera version where applicable
- Golden Sample
- QC requirement
- Packaging specification
- Previous production notes
This shortens decision time without eliminating verification.
New Material Lots Still Need Incoming Control
First Piece Is Reconfirmed
Approved Change Becomes the New Reference
The Network Supports Different Brand Operating Models
Automotive Accessory Brands
RV and Trailer Brands
Dealers and Distributors
Private-Label Brands
Large E-Commerce Programs

Verify the Manufacturing Network Before You Commit
Review a Real Product Route
Check Work-in-Process Identification
Review Approved References
Discuss Backup and Capacity Logic
Verify Repeat-Order Control
A mature supplier should be able to explain how a repeat PO reconnects to the previously approved product. The review should show how new material lots, first pieces and approved revisions are handled rather than assuming the previous result will reproduce itself automatically.

Frequently Asked Questions About Manufacturing Networks
Different tire cover programs depend on different bottlenecks. A new camera product requires engineering and fitment before scale, while a 5,000-piece Oxford program depends more on material planning, cutting, sewing and QC. Routing the project by its technical needs protects speed and consistency better than forcing everything through one standard line.
Yes. A project can separate artwork, printing, cutting, sewing, assembly, QC or packaging when that route is technically appropriate. Project ID, SKU, material lot, artwork version and QC status help keep the work controlled during the handoff.
Szoneier project management maintains customer specification control across the network. Individual functions own the quality of the process they perform, while the project system keeps material, artwork, pattern, camera, QC and packaging aligned with the approved product.
Controlled transfers can carry Project ID, customer, SKU, material lot, artwork version, quantity, QC status and next process. Printed panels, cut panels, blank covers and other work-in-process should remain identifiable rather than moving as anonymous material.
Eligible work can move to an approved backup route when equipment, capacity or delivery risk requires it. The alternative route must still meet the approved product and process requirements. Szoneier does not treat spare capacity as automatic technical approval.
For core materials, Szoneier’s supply-risk principle is to maintain at least two approved sourcing options where practical. Backup sourcing does not allow uncontrolled substitution; each material still has to meet the approved project requirement.
New camera-compatible products are developed through requirement review, fitment, pattern, prototype and camera verification. Bulk production starts only after the approved structure and Golden Sample are established, so volume manufacturing reproduces a proven configuration.
Szoneier uses modular capacity planning. Material, printing, cutting, sewing, QC, packaging and SKU complexity are reviewed to identify the real bottleneck. Additional cells, shifts, approved backup capacity or phased shipment can be used according to the program.
Repeat orders reopen the approved material, pattern revision, artwork, Golden Sample, QC requirement and packaging data. New material lots and first pieces are still verified, and approved changes become controlled new revisions rather than informal substitutions.
Yes. A supplier review can focus on the proposed program and examine product routing, samples, material approval, artwork/pattern control, work-in-process traceability, QC records, backup logic and repeat-order controls. The review is more useful when tied to a real product category.
CTA: Ask Network Question
CTA: Start Supplier Review

Plan the Manufacturing Route Before You Place the Order
- Product type and estimated quantity by SKU
- Vehicle, tire size and camera information where relevant
- Existing sample, drawing or technical specification
- Logo, artwork, photo or brand-color reference
- Preferred material, GSM, thickness or performance requirement
- Printing or decoration requirement
- Packaging, barcode, insert or private-label requirements
- Sample target and bulk delivery target
- Customer QC standard, AQL plan or third-party inspection need
- Reorder forecast, launch plan or annual volume estimate

